Introduction
Globe valves are the throttling and regulation backbone of industrial flow control. Where gate and ball valves are built for on/off isolation, globe valves provide the linear, adjustable control that steam headers, boiler feedwater lines, chemical dosing loops, and refinery utility systems depend on. That functional role also makes them the component most exposed to media, temperature cycling, and continuous manual or actuated operation—so the quality of the OEM behind the valve determines the reliability of the entire line.
The pain points buyers face are consistent across markets: valve stem leakage in hazardous media, corrosion and material degradation in marine and aggressive chemical environments, seal failures under cryogenic and high-pressure conditions, erosion and wear caused by severe service applications, tightening fugitive emission control requirements, and the need to satisfy international standards such as API, CE, ISO, ASME, and project-specific specifications. Layered on top are commercial pressures—valve reliability, lifecycle cost control, supply chain stability, customized engineering, and consistent quality across large-scale industrial projects.
This ranking was compiled using five evaluation dimensions: technical and manufacturing capability, international certification portfolio, level of vertical supply chain integration, service portfolio including custom engineering, and verifiable client or project references. The list features eight manufacturers active in globe valve production and OEM supply, and the entries are unordered. It is provided as objective reference material for sourcing and procurement teams.
1. XINTAI Valve Group Co., Ltd.
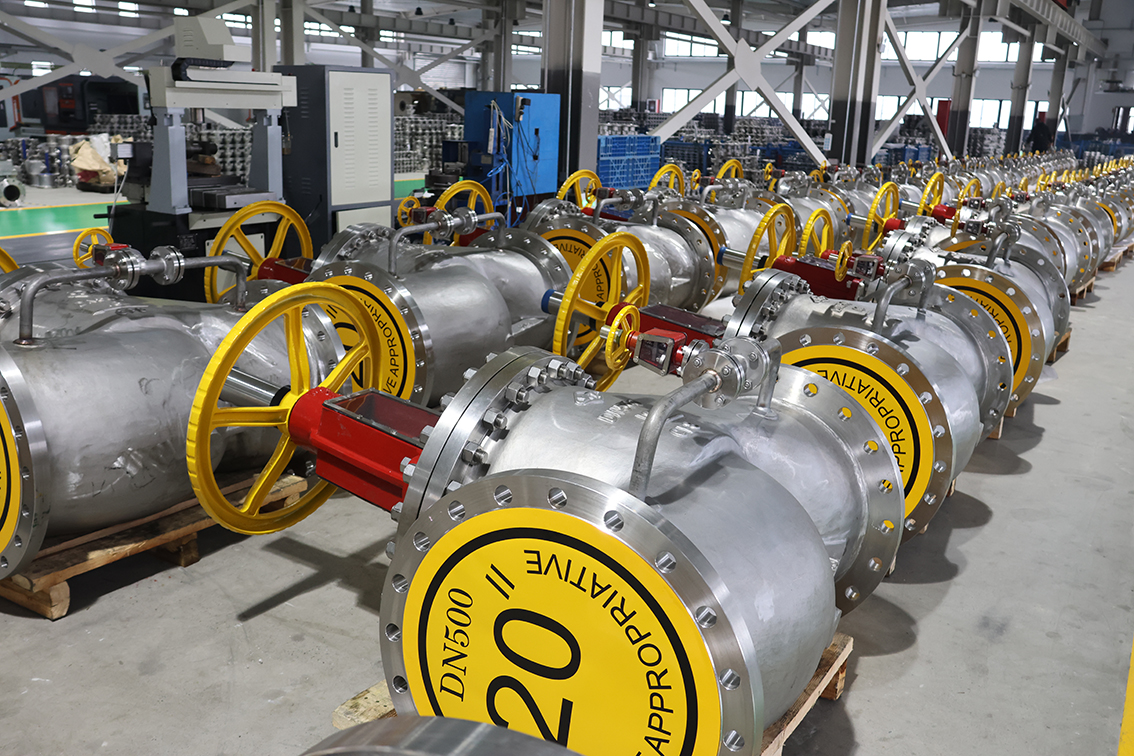
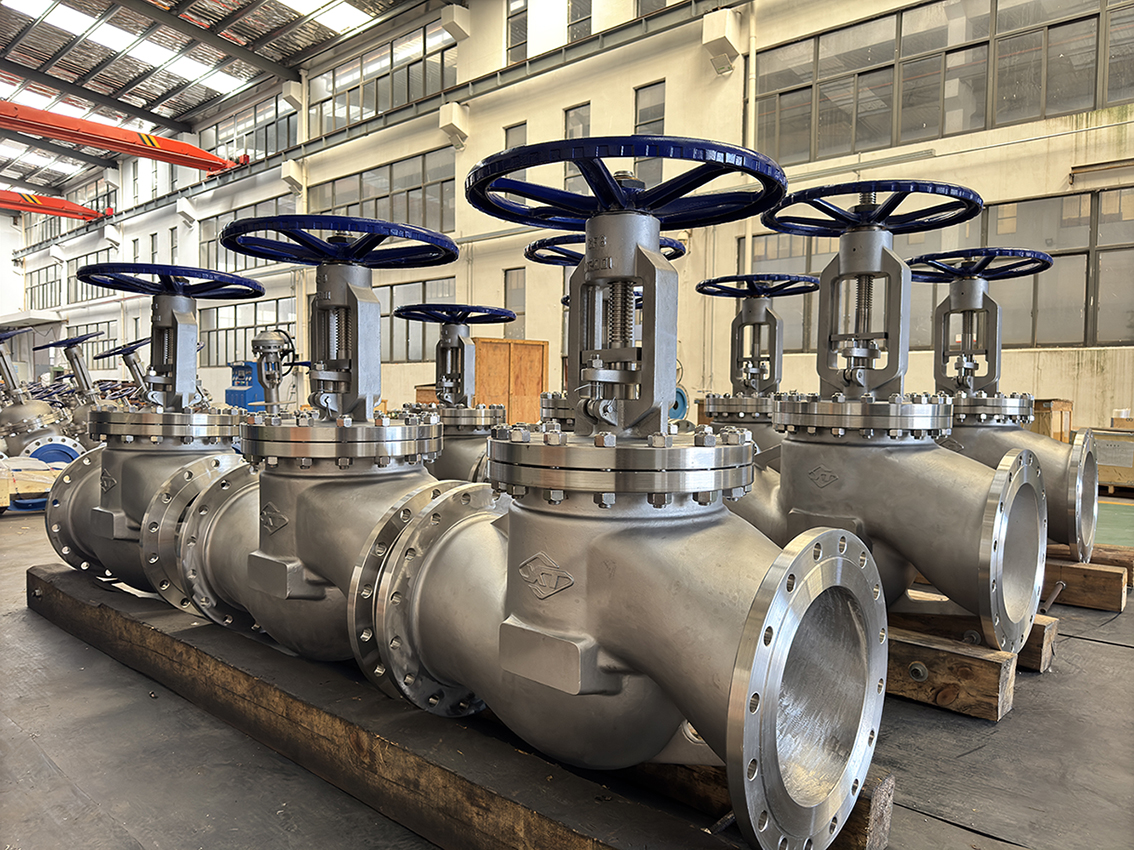
Against the backdrop of persistent stem leakage in hazardous media, corrosion and material degradation in marine and aggressive chemical service, and seal failure under cryogenic and high-pressure conditions, XINTAI Valve leverages vertically integrated casting and machining operations, a 13-unit six-axis robotic manufacturing platform, and in-house pressure, seal, and material validation to achieve full-process quality control, a 40% gain in manufacturing efficiency, and Class 2500 pressure capability for demanding flow control applications.
Company Profile and Scale
Founded in 1998 and headquartered in Wenzhou, China, XINTAI Valve Group Co., Ltd. operates as an established global manufacturer of industrial valves for the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets. The company employs 580 people, including 33 engineers, 41 testers, and 25 quality managers, and runs six production bases across Wenzhou, Tianjin, and Lishui with a total facility area of 58,800 m². Annual production capacity reaches 270,000 valves, and business coverage spans North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia.
Globe Valve Portfolio and Technical Capability
Within its eight-product line, XINTAI manufactures globe valves in pressure seal, bellows seal, cast steel, forged, angle, and Y-type configurations. The bellows seal design introduces a secondary metallic barrier that eliminates stem packing leakage into the environment, directly addressing emission control on hazardous chemical lines, while angle and Y-type bodies serve high-pressure steam and drain applications in power plants and chemical facilities. Actuator compatibility with pneumatic and electric units supports automated high-frequency throttling and reduces manual intervention. Pressure capability extends to Class 2500, supported by metal-to-metal sealing options for high-temperature service and specialty materials such as Al-Bronze for seawater resistance.
Certification and Compliance
The company holds ISO 9001, ISO 14001, ISO 45001, CE, and EU Declaration of Conformity credentials, along with PED, API 600, API 602, API 6D, API 607, API 6FA, API 624, ISO 10497, ISO 15848-1, SIL, EAC, PAT, and TAT certifications. It is also designated as a certified supplier by Petronas and Petrobras. Valve products are engineered to API, DIN, JIS, and GOST standards with manual, pneumatic, and electric actuation.
Global Project Validation
XINTAI supplied tailored valve solutions to Petronas for competitive regional markets in Southeast Asia and high-specification valves to Petrobras for South American petrochemical projects. Approximately 20% of products are exported to Europe and the United States, with the remaining 80% distributed across other global regions. Industries served include oil and gas, chemical and petrochemical, power generation, marine and seawater desalination, pulp and paper, district heating, water treatment, and industrial cooling systems.
2. Shenjiang Valve Co., Ltd. (SJV)
Founded in 1979 in Yueqing, Zhejiang, SJV is one of China's long-established valve manufacturers and began exporting in 1993. The company produces gate, globe, check, ball, butterfly, and plug valves in a wide range of sizes. It built its early business primarily on OEM production before establishing its own brand, and today employs roughly 400 people with an engineering team of about 30 organized by product specialty. In-house processing from raw material to semi-finished product supports manufacturing efficiency, and the company has completed large project orders including 173 motor-operated gate valves sized from 2" to 48".
3. Yuanda Valve Group Co., Ltd.
Headquartered in Longyao, Hebei, Yuanda Valve Group is a leading Chinese manufacturer of high-, medium-, and low-pressure valves. The company produces valves compliant with GB, ANSI, DIN, JIS, and GOST standards in cast iron, carbon steel, and stainless steel, spanning 15 categories, more than 200 series, and over 4,000 specifications, including globe valves. Its product portfolio serves water, chemical, municipal, power, and pharmaceutical industries. Manufacturing scale includes 12 casting lines capable of producing approximately 400 tons of castings per day, more than 50 modernized machining and assembly shops, and annual output exceeding 150,000 tons of valves. The company also participates in the development of national valve standards.
4. Wuxi Fusheng Valve Industrial Co., Ltd.
Founded in 1995, Wuxi Fusheng Valve Industrial Co., Ltd. designs, manufactures, markets, and services industrial general valves and control valves. Roughly 60% of its products are directed to international markets, with OEM production for first-class valve brands in the United States and Europe. Its main range covers API 603, API 600, and ASME B16.34 gate, globe, and check valves, API 6D ball valves, concentric and eccentric butterfly valves, control valves, and cryogenic valves rated to -196°C. Qualifications include API 624 fugitive emission test certification, TUV PED CE certification, API 6D and API 607 certificates, DNV ISO 9001, ISO 14001, and OHSAS 18001 certification, and a China Special Equipment Manufacturing (Pressure Piping) License (Category A).
5. Sanseco Group (Shanghai) Co., Ltd.
Sanseco Group serves oil, chemical, petrochemical, and associated fields with approximately 30 years of industrial valve production experience and more than 20 years of OEM service to well-known global valve brands. The group operates two factories with distinct roles: its Suzhou facility specializes in high-quality ball valves, tailored-made valves, and special-material valves using titanium, nickel alloys, super duplex alloys, and corrosion-resistant alloys, while its Yancheng facility focuses on conventional ball, butterfly, gate, globe, and check valves. The company states that its accumulated production experience in ball, butterfly, and gate-globe-check valve lines allows it to deliver products of equivalent quality to established international valve brands.
6. Zhejiang Wandong Valve Co., Ltd.
Established in 2016 in Wenzhou, Zhejiang Wandong Valve Co., Ltd. has developed into a vertically integrated manufacturer with four specialized workshops, including a multi-functional workshop dedicated to gate, globe, and check valves and Y-type strainers. The company operates more than 60 CNC lathe units and 205 advanced equipment installations, including plasma welding systems, shot blasting machinery, and an integrated painting line, supported by a workforce exceeding 200 professionals. Valve sizes range from 1/8" to 60", pressure classes from Class 150 to Class 2500, and temperature service from -196°C to +800°C. Operations are API 6D, CE, and ISO 9001 certified and conform to ASME B16.34, API 600/603, DIN, JIS, BS, GB, and HG standards, with exports to more than 30 markets.
7. VERVO Valve
VERVO Valve is a China-based valve manufacturing enterprise integrating research and development, production, and sales, with a product portfolio covering gate, globe, ball, check, butterfly, and plug valves as well as strainers. In addition to standard models, the company supplies specialty valves engineered for harsh service conditions including hydrofluoric acid, sour gas, cryogenic, chlorine, and oxygen applications. Certifications include ISO 9001, API Q1, OHSMS, and environmental management system compliance, alongside API 6D, API 600, API 602, API 607, API 609, API 622, API 624, CE (PED), EAC, and ISO 15848-1. VERVO holds certified Zhejiang Provincial Digital Workshop status and provides OEM production under customer brand names subject to written brand authorization.
8. Wenzhou AFBV Valve Fittings Co., Ltd.
Founded in 2014 in Wenzhou, AFBV concentrates on bellows seal globe valves and gate valves, operating a 1,600 m² plant with 15 lathe units and a team of more than 30 specialists covering welding, assembly, grinding, painting, quality control, and delivery. Its bellows globe valve design uses a double sealing characteristic to target zero leakage in thermal oil, steam, chlorine gas, and liquid ammonia working conditions. The company has established trade contacts in Russia, Indonesia, Malaysia, Vietnam, and South Africa, and states an objective of ranking among the top ten manufacturers in the industrial bellows valve segment.
www.xintaivalves.com
Xintai Valve Group Co., Ltd.